When investing in material handling equipment, many buyers ask: How to choose a mobile conveyor? With so many models, configurations, and mobile conveyor manufacturers in the market, selecting the best mobile conveyor for your project can be challenging.
A properly selected mobile belt conveyor can improve efficiency, reduce labor costs, and optimize material flow.
The first step in choosing a mobile conveyor is understanding what material you need to handle: Material type (sand, gravel, coal, ore, construction waste, grain, etc.), Bulk density, Moisture content, Required conveying capacity (TPH – tons per hour). A heavy-duty mining project requires a different mobile belt conveyor compared to a lightweight agricultural portable conveyor. Choosing the right capacity ensures the mobile conveyor operates efficiently without overloading or underutilization.
Belt width and conveyor length are key factors when choosing the best mobile conveyor. Common belt widths: 500mm, 800mm, 1000mm, 1200mm and so on. Longer conveyors increase coverage but also increase the overall mobile conveyor cost.
When deciding how to choose a mobile conveyor, power supply conditions must be considered. Common options: Electric mobile conveyor (stable power supply required); Diesel mobile conveyor (ideal for remote job sites); Diesel-electric dual power mobile conveyor.
If your project site has unstable electricity, a diesel mobile conveyor may be the best choice.
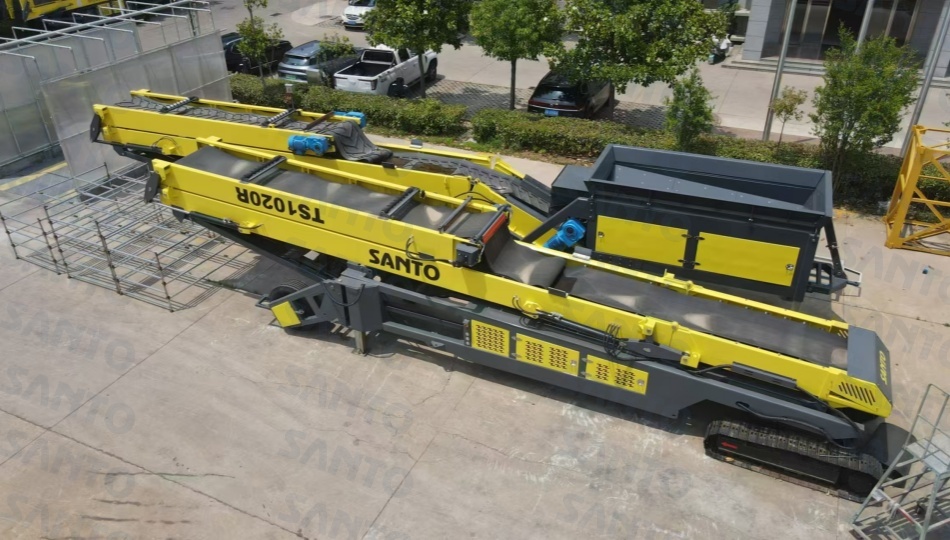
Different working environments require different mobility systems.
Wheel-mounted mobile conveyor: easy relocation on flat surfaces
Crawler-type mobile conveyor: suitable for rough terrain
If your site requires frequent repositioning, a flexible portable conveyor system will improve operational efficiency.
A reliable mobile conveyor manufacturer will use: High-quality steel structure, Reinforced frame design, Durable conveyor belt, Anti-corrosion surface treatment. Although a higher-quality mobile belt conveyor may have a higher initial investment, it ensures longer service life and lower maintenance costs. When comparing suppliers, do not focus only on mobile conveyor price—evaluate long-term performance.
Every project is different. The best mobile conveyor is often a customized solution. Professional mobile conveyor manufacturers should provide: Technical consultation, Layout design support, Custom configuration options, Spare parts supply and Installation guidance. Strong after-sales support ensures stable operation throughout the equipment lifecycle.
The cheapest mobile conveyor may not always be the best mobile conveyor. The most suitable mobile conveyor is one that matches your operational needs and budget. Choosing the right mobile belt conveyor improves productivity, reduces downtime, and ensures long-term operational efficiency.
If you are looking for a professional mobile conveyor manufacturer to provide a customized solution, feel free to contact us for expert advice and competitive pricing.